ENGINEER-TO-ORDER · PROCESS STANDARDIZATION
Your ETO Backlog Isn't a Capacity Problem.
It's a Repetition Problem.
The bottleneck is rarely the number of engineers. It is the number of times the same engineering decision gets rebuilt from zero.
THE REAL ISSUE
Adding headcount does not remove repeated work.
Most service body and specialty vehicle manufacturers treat Engineer-to-Order backlog as a headcount issue. Add another designer, add another checker, throw more hours at the queue. It doesn't work, because the bottleneck was never the number of engineers — it was the number of times the same decision got re-engineered from zero.
If your ETO desk is averaging 50–60+ hours per order, you don't have a staffing gap. You have a standardization gap, and it's compounding with every PO that comes in.
WHERE THE BUDGET LEAKS
Where the Hours Actually Go
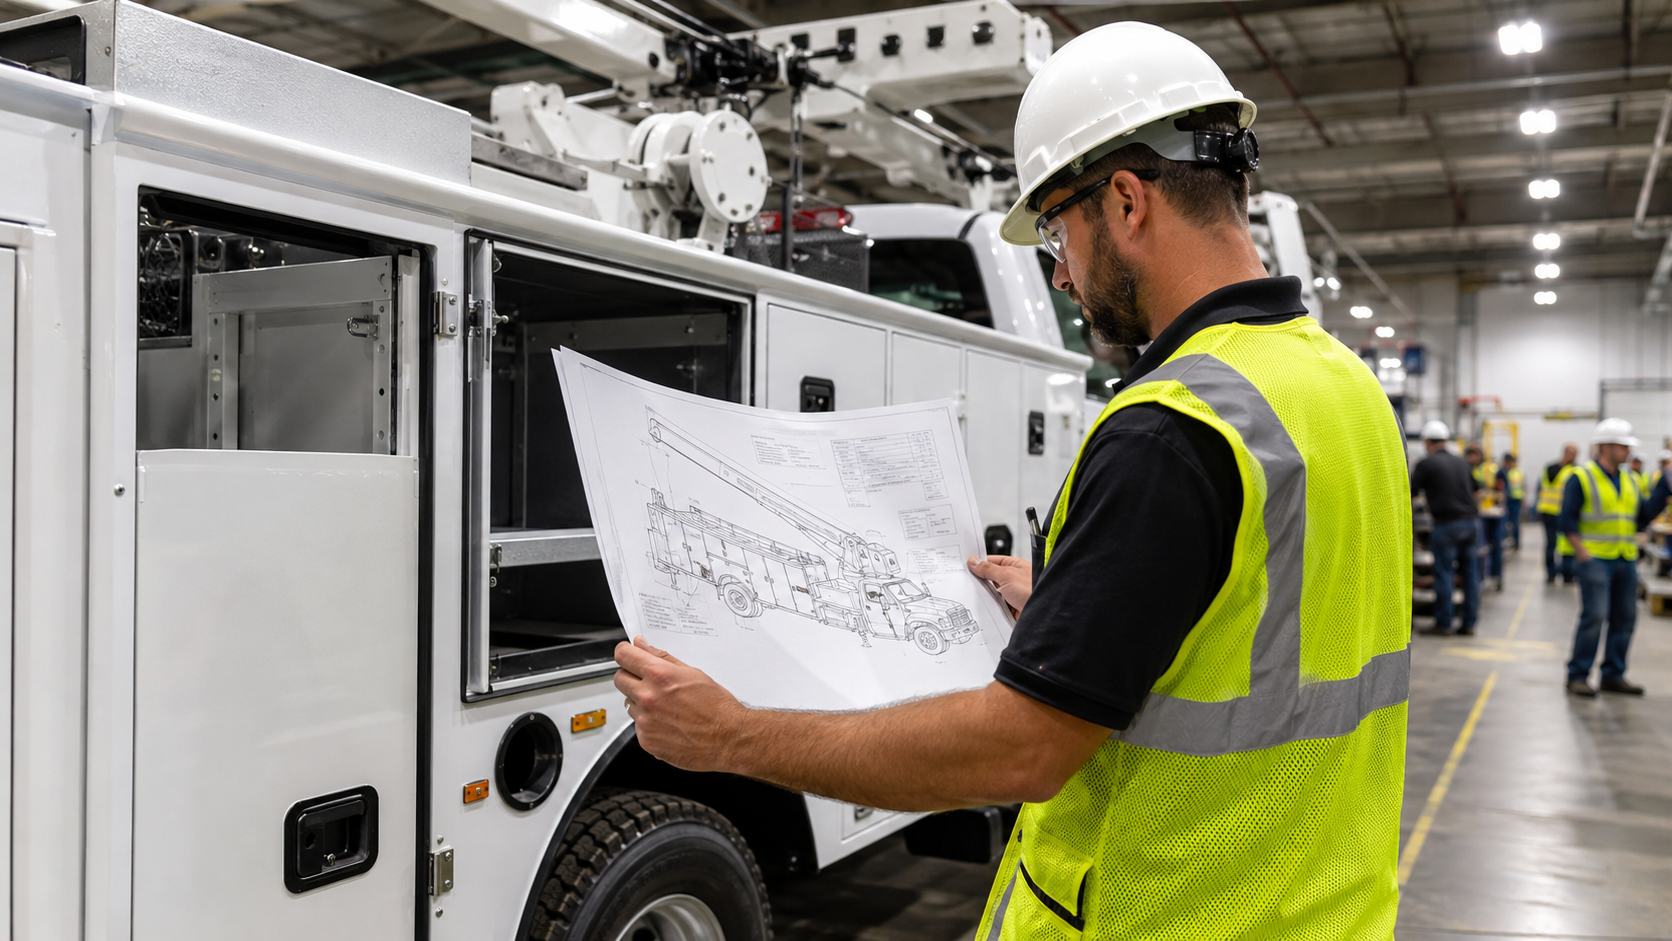
Pull apart a typical ETO cycle for a bucket truck, service body, or utility chassis upfit and the time breaks down roughly like this:
None of this is a skills problem. Every order resets the clock to zero instead of starting from a known-good baseline.
Where ETO Hours Get Consumed
JAYDU'S APPROACH
What Actually Fixes This
We worked this exact problem with a leading North American service truck manufacturer carrying a heavy ETO backlog. The fix wasn't more headcount — it was rebuilding how ETO orders move through engineering.
Build a standard component library before touching the backlog.
Every recurring chassis configuration, compartment module, hydraulic assembly, and electrical schematic pattern got pulled into a reusable library. A new order becomes a configuration exercise against proven components, not a blank-sheet design.
Separate “standard” from “custom” at intake, not at the end.
We classified order options at intake — which elements are configurable from the library, and which actually require new engineering. That single triage step removes most orders from the “full redesign” path before a drawing is even opened.
Move FEA earlier, not later.
Running Ansys validation in parallel with GA development — instead of as a final gate — catches structural conflicts while they're still cheap to fix.
Build GA and electrical schematics together, not sequentially.
Designing layout and routing in the same pass eliminates the rework loop where a downstream layout change forces an upstream schematic rebuild.
Deploy a dedicated team against the backlog specifically.
A ring-fenced team against the backlog — separate from day-forward order processing — is what actually brings the number down, instead of new work perpetually winning the priority fight.
THE JAYDU ETO RECOVERY FRAMEWORK
Five connected steps that stop the reset-to-zero cycle.
Triage at Intake
Classify orders as standard configurations or true custom engineering.
Build the Engineering Library
Create reusable chassis, compartment, hydraulic, and electrical modules.
Run FEA in Parallel
Validate structural integrity during design instead of after documentation.
Integrate GA and Electrical Design
Develop layouts and wiring simultaneously to eliminate rework.
Deploy Dedicated Backlog Capacity
Separate backlog processing from day-forward engineering operations.
IMPLEMENTATION MAP
From activity to measurable business impact.
| Step | Activity | Jaydu's Role | Business Impact |
|---|---|---|---|
| 1 — Triage | Classify order options at intake | Standard vs. custom split applied to every PO | Most orders removed from the full-redesign path |
| 2 — Library Build | Compile recurring components, GA blocks, and schematics | Reusable component and drawing library created | New orders configured instead of redesigned |
| 3 — Parallel FEA | Run Ansys validation during design, not after | Structural validation built into the design pass | Conflicts identified earlier when they are easier to resolve |
| 4 — Integrated Design | Develop GA and electrical schematics together | Single coordinated design workflow | Reduced downstream engineering rework |
| 5 — Dedicated Team | Ring-fenced team focused exclusively on backlog work | Dedicated engineering capacity deployed against backlog | Backlog cleared without disrupting day-forward orders |
An engineering process that scales with demand—not just a backlog reduction project. The manufacturer gained a repeatable ETO workflow capable of supporting future order growth without reintroducing the same bottlenecks.
THE COMMON MISTAKE
Why Most Internal Fixes Don't Get There
We see manufacturers attempt this internally and stall for a predictable reason: building a standard library and a triage process takes dedicated engineering time — time that doesn't exist, because every available hour is already going toward the current backlog. It's the same trap as fixing a process while running the line at full output.
The other failure mode: companies build a component library but never enforce the intake triage. Under deadline pressure, engineers default back to full custom design, and the library quietly goes unused. The library and the triage discipline have to be deployed together, or the gains don't hold.
READY TO CLEAR YOUR BACKLOG?